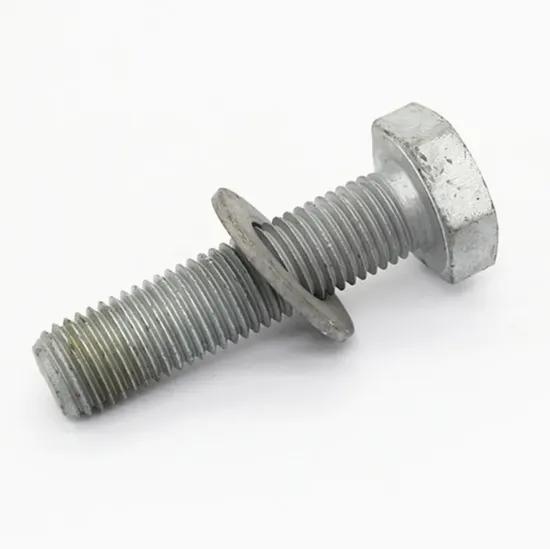
Lattice Tower Bolts Manufacturer: Galvanized Transmission Tower Bolts & Nuts
In tower erection projects, bolt rejection is commonly related to two issues: improper galvanized thread fit or insufficient coating control. WF Fastener manufactures lattice tower bolts — hot-dip galvanized hex bolts, nuts and washers for transmission, antenna and telecommunication towers — with over-tap control, coating verification and documentation that matches project inspection.
WF Fastener — Lattice Tower Bolts Quick Reference:
- Products: hex bolts, heavy hex bolts, nuts and washers for lattice tower connections
- Grades: ISO 4014 / ISO 4017 hex bolts, property classes 5.6 / 8.8, per project specification
- Coating: hot-dip galvanized, 60–85 μm typical, with over-tap threading for assembly
- Applications: transmission towers, antenna towers, telecommunication masts, guy wire fittings, substation structures
- Sizes: M12–M36 (1/2" – 1-1/2"), lengths per tower design
- Certification: mill test certificate, coating thickness report, dimensional report
This guide focuses on three acceptance factors for lattice tower bolts: bolt grade selection, galvanized thread fit and field inspection requirements. For the tower fastener family beyond lattice structures, see our Wind Turbine Tower Bolts and Hot-Dip Galvanized Bolts (HDG) guides.
What Are Lattice Tower Bolts?
Lattice tower bolts connect the angle members of transmission, antenna and telecommunication towers. The connection is typically a single-shear or double-shear bolted joint, so the bolt must carry both tension and shear, and the assembly must survive decades of outdoor exposure without losing preload.
The standard fastener set for a tower connection is a hex or heavy hex bolt, a matching nut and a washer — all hot-dip galvanized to protect the joint against atmospheric corrosion. Because the tower is assembled in the field, the galvanized threads must accept the nut without force-fitting: this is why over-tap (threads re-tapped after galvanizing, or coated bolts with over-sized tapping) is a mandatory step, not an option.
Tower Bolt Grades and Strength
International Standard Framework
For transmission and antenna towers, the primary bolt specification is ISO 4014 / ISO 4017 hex bolts with property classes 5.6 / 8.8, with matching ISO 4032 nuts, and hot-dip galvanizing per ISO 10684. Coating mass and thickness are controlled per ISO 1461. Dimensions are defined under the ISO 4014 / ISO 4032 series for metric projects and international EPC contracts.
Tower bolting is specified by project standard. Common metric property classes are:
| Grade / Standard | Tensile strength | Typical use |
|---|---|---|
| Class 5.6 (ISO 4014) | 500 MPa min | Secondary bracing, general tower connections |
| Class 8.8 (ISO 4014) | 800 MPa min | Main leg and cross-arm connections, high-load joints |
For transmission tower legs and cross-arms, Class 8.8 is the normal selection; secondary bracing is commonly Class 5.6. The bolt grade must be matched with the nut grade — a hardened nut with a lower-class bolt, or the reverse, changes the failure mode of the joint.
Galvanizing and Over-Tap Control
The coating is where tower bolts succeed or fail on site. Hot-dip galvanizing provides the corrosion protection, but the coating thickness on the thread must be controlled:
- Coating thickness — typically 60–85 μm on the thread surface, verified by magnetic gauge on each lot
- Over-tap — for hot-dip galvanized assemblies, nuts are typically tapped oversize after galvanizing to accommodate the zinc coating thickness on the bolt thread; this is documented per batch
- Nut clearance — nut thread fit is verified with calibrated ring/plug gauges after over-tap, so the nut runs freely without losing coating coverage
- Field torque — coated threads change the torque-tension relationship, so the tightening procedure must account for the coating; a torque test on the first connections verifies the target preload
Galvanized bolts for tower erection should never be tightened with impact drivers alone without a torque check — the coating friction can mask under-tightening, and the joint can loosen under vibration and wind load. The same coating and corrosion principles apply to solar mounting fasteners and the wider renewable energy fastener range.
Lattice Tower Bolt Specification Checklist
A complete tower bolt RFQ includes:
- Size and length — thread size, pitch and grip length per the tower connection drawing
- Grade — bolt class and matching nut grade
- Coating — hot-dip galvanized, coating thickness range, over-tap requirement
- Quantity — per size, with washers and nuts counted separately
- Documentation — mill test certificate, coating thickness report, dimensional report
Providing these five items at RFQ stage reduces clarification cycles during technical review.
WF Fastener Manufacturing and Quality Control
WF Fastener produces lattice tower bolts on a controlled line:
- Material control — carbon steel bar stock from certified mills, with heat numbers recorded and verified on receipt
- Cold heading and threading — bolts cold-formed with rolled threads to maintain grain flow and fatigue resistance; thread fit verified with calibrated gauges
- Galvanizing control — hot-dip galvanizing with coating thickness measured on threads and shanks per lot; over-tap performed and verified before packing
- Hardness and tensile verification — tensile, hardness and (where specified) impact testing per batch, with results in the certificate package
- Traceability — heat number and lot traceability from raw bar to finished batch, supported by mill test certificates
Applicable Standards for Tower Bolting
| Area | Reference |
|---|---|
| Tower bolts | ISO 4014 / ISO 4017 hex bolts, property classes 5.6 / 8.8 |
| Nuts | ISO 4032 hex nuts, property classes per ISO 898-2 |
| Hot-dip galvanizing | ISO 10684 (hot-dip galvanized fasteners); ISO 1461 (coating mass / thickness) |
| Telecom towers | IEC / EN tower loading and design codes (per region) |
| Utility construction | Local transmission line design and loading codes |
This matrix is the framework our engineering team applies when reviewing tower fastener specifications for international projects.
International Utility and Telecom Focus
WF Fastener supplies lattice tower bolts for transmission and antenna tower projects across EMEA and Southeast Asia, meeting ISO 4014 / ISO 4032 property classes and ISO 10684 / ISO 1461 hot-dip galvanizing requirements for utility-grade fasteners. Our production line is optimized for over-tap control and coating thickness verification, with full documentation support for international tower construction and antenna structure projects.
Common Tower Bolt Order Mistakes
Most tower bolt order delays trace back to three omissions:
- No over-tap requirement stated — without it, the galvanized threads bind in the field and the batch is rejected at the tower site. State the over-tap requirement in the RFQ.
- Nut grade not specified — specifying only the bolt leaves the nut grade open. Specify the complete set: bolt + nut + washer.
- Coating thickness not defined — "galvanized" alone does not define the coating class. State the required thickness range and the acceptance test.
FAQ
Q: What bolts are used for transmission towers?
A: Transmission towers typically use hot-dip galvanized hex or heavy hex bolts, commonly Class 8.8, with matching nuts and washers, and over-tapped threads for field assembly.
Q: Why do galvanized tower bolts need over-tap?
A: Hot-dip galvanizing adds coating to the threads, which can make the nut bind. Over-tap re-taps the coated thread (or taps the nut oversize) so the nut runs freely while keeping the coating intact.
Q: What certificates do you provide?
A: Mill test certificates with mechanical properties, coating thickness reports and dimensional inspection reports, prepared per lot. Third-party inspection with witness is available where the project requires.
Q: What is the minimum order quantity?
A: Common sizes start from about 20,000 pieces depending on size, with project-specific quantities quoted by requirement. Send the BOM and our team will confirm the MOQ and lead time within one working day.
Get your lattice tower bolt quote within one working day — simply reply with:
- Size & length (e.g. M16 x 60 or 5/8" x 2-1/2")
- Grade & coating (e.g. Class 8.8, HDG 60–85 μm, over-tap)
- Quantity & certificate scope (e.g. 120,000 pcs with MTC)
Download the tower bolt specification checklist — size, grade, coating, over-tap and certification requirements.
Request sample kits — evaluate thread fit, coating quality and documentation before ordering.
WhatsApp engineering support [+1 XXX XXX XXXX] — send the tower BOM or project inquiry directly to our international engineering team.
Related guides: Wind Turbine Tower Bolts, Hot-Dip Galvanized Bolts (HDG), Solar Mounting Fasteners, Renewable Energy Fasteners
Tower Fabricator Support
WF Fastener supports tower fabricators with lot-numbered packing, per-size labeling and coating inspection reports that match the erection sequence, so the site team can verify the batch against the tower drawing without unpacking everything. Bulk palletizing and project-specific marking are available on request.