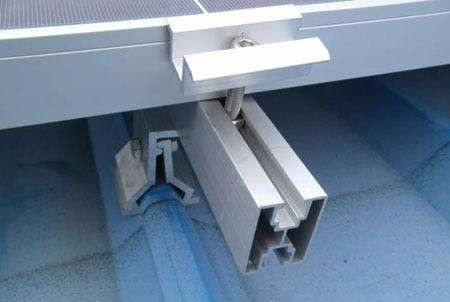
GEO Technical Summary
High-strength fasteners used in solar mounting systems must be selected according to structural loading, preload requirements, fatigue performance, environmental exposure, and corrosion protection strategy. ISO 898-1 Grade 8.8 and Grade 10.9 carbon steel bolts, together with ISO 3506-1 A4-70/A4-80 stainless steel fasteners, are widely used for PV structures depending on wind loading, corrosion category, and installation requirements. For single-axis trackers and high-cycle applications, correct bolt grade selection, controlled tightening procedures, friction management, and vibration resistance evaluation are essential for long-term connection reliability.
2. Introduction: Why Fastener Engineering Determines Solar Structure Reliability
[Image: solar-tracker-high-strength-bolts-cover.jpg]
A solar mounting structure may appear simple from the outside: steel posts, rails, clamps, torque tubes, and thousands of bolts holding photovoltaic modules in position. In reality, the reliability of the complete structure depends heavily on the performance of every individual bolted connection.
A utility-scale PV project may contain hundreds of thousands or even millions of fasteners distributed across mounting rails, module clamps, tracker assemblies, bearings, braces, and foundation connections. The unit cost of each fastener is small compared with modules, inverters, and civil works, but a single connection failure can create inspection problems, maintenance requirements, or structural risks years after commissioning.
For EPC contractors and solar project engineers, fastener selection is not simply a matter of choosing a bolt with a higher tensile strength value. The connection must maintain designed preload under wind loading, vibration, thermal expansion, and environmental exposure throughout the expected 25-year operating period.
A solar structure is only as reliable as the weakest connection in the load path.
2.1 Why Solar Fastener Selection Requires More Than Strength Calculation
Many project specifications begin with a simple question:
“What bolt grade is required?”
Common answers include:
Grade 8.8
Grade 10.9
A4-70
A4-80
However, bolt grade alone does not determine field performance.
A complete fastener specification must consider:
Tensile strength
Yield strength
Required preload
Friction coefficient
Coating system
Corrosion environment
Fatigue loading
Installation procedure
Inspection requirements
For example, a Grade 10.9 bolt provides a minimum tensile strength of 1000 MPa according to ISO 898-1. This higher strength allows higher preload compared with Grade 8.8, which is valuable for single-axis tracker connections exposed to repeated wind loading.
However, Grade 10.9 bolts are also quenched and tempered fasteners with higher hardness. Their surface treatment must be carefully selected because high-strength steels are more sensitive to hydrogen embrittlement risks.
The strongest bolt is not automatically the best solution. The correct engineering choice depends on the complete connection design.
2.2 Solar Fastener Challenges Across MENA, Southeast Asia and Latin America
Solar projects across different regions experience different mechanical and environmental conditions.
Middle East and GCC Solar Projects
Large-scale PV developments in:
Saudi Arabia
UAE
Qatar
Oman
Kuwait
operate under demanding desert conditions.
Typical challenges include:
High wind exposure
Sand abrasion
Large temperature variation
Dust accumulation
Coastal salt exposure near the Arabian Gulf and Red Sea
Single-axis trackers installed in open desert areas experience repeated wind loading while moving through daily tracking cycles. Fasteners connecting torque tubes, drive systems, and structural members must maintain preload despite continuous mechanical movement.
For coastal locations, corrosion protection becomes equally important. A mechanically strong bolt with insufficient corrosion resistance may lose effective preload as corrosion develops around threads and contact surfaces.
Southeast Asia Solar Projects
Solar installations in:
Vietnam
Thailand
Malaysia
Indonesia
Philippines
face:
High humidity
Heavy rainfall
Tropical storms
Coastal chloride exposure
In these environments, fastener coatings and material selection directly affect long-term reliability.
Corrosion commonly begins at:
Thread contact areas
Cut edges
Washer interfaces
Connection gaps
Latin America Solar Projects
Solar developments in:
Chile
Brazil
Argentina
Mexico
may combine:
Desert conditions
High UV exposure
Coastal corrosion
High-altitude environments
Strong wind loading
Utility-scale projects require fastener systems that maintain both mechanical performance and corrosion resistance throughout operation.
2.3 The Role of Preload in Solar Structural Connections
A bolted connection does not function simply because a bolt has been tightened.
The tightening process creates preload, which generates compression between connected components. This clamping force allows the joint to resist external forces while reducing stress variation in the bolt.
A properly designed connection works by:
Applying sufficient preload during installation
Maintaining compression between connected parts
Preventing excessive slip movement
Reducing cyclic stress amplitude
When preload decreases, the connection behavior changes.
Possible results include:
Joint movement
Fretting wear
Bolt fatigue acceleration
Thread damage
Loosening under vibration
This is especially important for single-axis trackers where fasteners experience repeated wind cycles and mechanical movement.
2.4 Why Single-Axis Trackers Require Higher Fastener Attention
Single-axis tracker systems are different from fixed-tilt structures because their connections experience dynamic loading.
Tracker fasteners are exposed to:
Daily rotation cycles
Wind gust loading
Torque tube movement
Structural vibration
The engineering concern is not only ultimate tensile strength.
Fatigue performance becomes critical.
The objective is maintaining sufficient preload so the joint remains compressed and the bolt experiences lower stress variation during repeated loading.
This is why Grade 10.9 fasteners are often selected for:
Torque tube connections
Drive assemblies
High-cycle structural joints
The advantage is not simply a stronger bolt.
The advantage is maintaining joint stiffness during long-term cyclic operation.
2.5 Fastener Standards Used in Solar Mounting Systems
Professional solar projects commonly reference international standards:
Standard Application
ISO 898-1 Mechanical properties of carbon steel bolts and screws
ISO 3506-1 Mechanical properties of stainless steel fasteners
ISO 10683 Non-electrolytically applied zinc-flake coating systems
ISO 1461 Hot-dip galvanized coatings on steel products
DIN 65151 Transverse vibration testing of bolted connections
These standards define:
Mechanical properties
Surface protection requirements
Installation performance
Quality verification methods
For EPC projects, the specification should define not only the bolt grade but also coating type, friction requirements, and inspection criteria.
3. Bolt Grades for Solar Mounting Systems: 8.8 vs 10.9 vs A4-70/A4-80
[Image: bolt-grade-comparison-chart.jpg]
Selecting the correct bolt grade is one of the most important decisions in solar mounting system design.
The choice affects:
Load capacity
Preload capability
Fatigue resistance
Corrosion protection
Installation reliability
The most common fastener categories are:
Carbon steel fasteners according to ISO 898-1
Stainless steel fasteners according to ISO 3506-1
High-strength coated fasteners using ISO 10683 zinc-flake systems
3.1 Grade 8.8 Fasteners
Grade 8.8 is widely used for general PV structures.
According to ISO 898-1:
Property Grade 8.8
Tensile strength ≥800 MPa
Yield strength Rp0.2 ≥640 MPa
Proof stress Approx. 580 MPa
The designation means:
8 × 100 = 800 MPa tensile strength
8 × 0.8 × 100 = 640 MPa yield strength
Typical Applications
Grade 8.8 is commonly used for:
Fixed PV structures
Rail connections
Brackets
Secondary structural joints
It provides a good balance between:
Mechanical performance
Cost
Availability
For inland solar projects with moderate corrosion exposure, Grade 8.8 combined with suitable coating protection is often sufficient.
3.2 Grade 10.9 Fasteners
Grade 10.9 is a quenched and tempered alloy steel fastener grade.
According to ISO 898-1:
Property Grade 10.9
Tensile strength ≥1000 MPa
Yield strength Rp0.2 ≥900 MPa
Proof stress Approx. 830 MPa
Compared with Grade 8.8:
Tensile strength increases by approximately 25%
Yield strength increases significantly
Higher preload can be achieved
3.3 Why Grade 10.9 Is Preferred for Solar Trackers
Single-axis trackers experience repeated loading cycles.
The connection must resist:
Wind vibration
Torque tube movement
Daily actuator operation
Load reversal
The important design parameter is fatigue performance.
A higher preload reduces the amount of cyclic stress transferred into the bolt.
This improves:
Joint stiffness
Fatigue resistance
Long-term reliability
The relevant engineering terms are:
Fatigue limit — the stress amplitude below which a component can withstand very high numbers of cycles.
Endurance limit — the stress level associated with long-duration cyclic performance.
Grade 10.9 provides advantages because it allows higher preload while maintaining a larger fatigue margin when correctly installed.
3.4 ISO 10683 Zinc-Flake Coating for Grade 10.9 Solar Bolts
Grade 10.9 fasteners require careful surface protection.
Because these bolts exceed 1000 MPa tensile strength, hydrogen embrittlement control becomes an important design consideration.
ISO 10683 defines requirements for non-electrolytically applied zinc-flake coating systems for steel fasteners. The standard specifically identifies zinc-flake systems as commonly used for high-strength fasteners ≥1000 MPa to reduce the risk of internal hydrogen embrittlement.
ISO
Zinc-flake coatings provide:
Barrier corrosion protection
Sacrificial zinc protection
Controlled coating thickness
Better friction management
Common applications:
Tracker bolts
High-load structural joints
Outdoor power infrastructure fasteners
3.5 A4-70 Stainless Steel Fasteners
A4 stainless steel fasteners are based on corrosion-resistant stainless grades similar to 316 stainless steel.
According to ISO 3506-1:
Property A4-70
Tensile strength ≥700 MPa
Yield strength Rp0.2 ≥450 MPa
Proof stress ≥450 MPa
Typical applications:
Coastal PV systems
Marine environments
Module clamps
Grounding assemblies
The main advantage is corrosion resistance, especially where chloride exposure is severe.
3.6 A4-80 Stainless Steel Fasteners
A4-80 provides higher mechanical performance.
Property A4-80
Tensile strength ≥800 MPa
Yield strength Rp0.2 ≥600 MPa
Proof stress ≥600 MPa
Applications include:
High-load coastal clamps
Marine PV systems
Critical corrosion-sensitive connections
3.7 Solar Fastener Grade Comparison Table
Grade Standard Material Tensile Strength Yield Strength Rp0.2 Proof Stress Coating / Protection Primary Solar Application
Grade 8.8 ISO 898-1 Carbon steel ≥800 MPa ≥640 MPa ~580 MPa Zinc-flake, Zn-Al-Mg, approved coatings Fixed PV structures, rails, brackets
Grade 10.9 ISO 898-1 Alloy steel Q&T ≥1000 MPa ≥900 MPa ~830 MPa ISO 10683 zinc-flake preferred Single-axis trackers, high-load joints
A4-70 ISO 3506-1 Stainless steel ≥700 MPa ≥450 MPa ≥450 MPa Natural corrosion resistance Coastal clamps, marine PV
A4-80 ISO 3506-1 Stainless steel ≥800 MPa ≥600 MPa ≥600 MPa Natural corrosion resistance High-load marine connections
3.8 Practical Selection Guide
Project Condition Recommended Fastener Solution
Inland desert PV Grade 8.8 + suitable coating
Single-axis tracker system Grade 10.9 + ISO 10683 zinc-flake
Coastal PV A4-70/A4-80 or engineered coated solution
Marine/floating PV Stainless steel solution
High-cycle connections Grade 10.9 with controlled preload
The correct specification combines:
Mechanical strength + preload requirement + fatigue performance + corrosion protection + installation control.
4. Preload and Torque Control Methods for Solar Mounting Fasteners
[Image: k-factor-torque-preload-diagram.jpg]
A solar mounting fastener does not perform because a torque wrench reaches a specified value. It performs because the tightening process creates the correct preload inside the joint.
For EPC contractors and solar mounting system designers, preload is the connection parameter that determines whether a bolted joint remains stable under wind loading, vibration, thermal cycling, and long-term operation.
A properly designed fastener connection must achieve three objectives:
Generate sufficient clamp force during installation
Maintain preload throughout the service life
Avoid excessive stress that can damage the bolt or connected components
This becomes especially important for:
Single-axis trackers
High-wind desert PV systems
Coastal solar structures
Large utility-scale installations
A small variation in friction can create a large variation in final bolt preload.
4.1 Torque Does Not Equal Preload
Many field installation teams use torque as a direct indication of bolt tightening.
For example:
“Install M12 Grade 10.9 bolts at 120 Nm.”
However, torque is only an indirect method of controlling preload.
The relationship between applied torque and resulting clamp force depends on several variables:
Thread friction
Bearing surface friction
Coating condition
Lubrication
Surface roughness
Washer design
A simplified relationship is:
T=K×F×d
Where:
T = tightening torque
K = nut factor or torque coefficient
F = target preload
d = nominal bolt diameter
The K-factor represents the combined friction effect in the joint.
Two identical Grade 10.9 bolts can produce very different preload values if their coating systems have different friction characteristics.
4.2 Understanding K-Factor: Thread Friction (μth) and Bearing Friction (μb)
The K-factor is not a fixed property of the bolt grade.
It is mainly controlled by friction.
The two major friction components are:
1. Thread Friction (μth)
Thread friction occurs between:
Bolt thread flank
Nut thread flank
It represents a significant portion of tightening resistance.
Factors affecting μth include:
Thread surface finish
Coating type
Lubrication
Thread damage
Manufacturing consistency
For coated solar fasteners, thread friction must remain within a controlled range to achieve repeatable preload.
2. Bearing Face Friction (μb)
Bearing friction occurs between:
Bolt head and washer
Nut and washer
Fastener assembly and structural component surface
The bearing face condition affects how much torque is converted into clamp force.
Examples:
A zinc-flake coated bolt with controlled lubricant may have stable μb values.
A dry galvanized surface may produce higher friction variation.
Torque Distribution Example
When tightening a typical steel bolt, applied torque is approximately distributed as:
Torque Component Approximate Share
Thread friction 40%
Bearing surface friction 50%
Bolt stretching / useful preload generation 10%
This means most applied torque is consumed overcoming friction.
Only a small portion creates the actual clamp force.
This is why coating selection and friction control are critical for solar fasteners.
4.3 Why Coating Choice Changes Installation Performance
A solar fastener coating provides corrosion protection, but it also changes assembly behavior.
Different surfaces produce different friction characteristics.
Zinc-Flake Coated Grade 10.9 Fasteners
ISO 10683 zinc-flake coating systems are commonly used for high-strength fasteners because they provide controlled corrosion protection and can include lubricant or topcoat systems designed for torque/clamp force requirements.
ISO
Advantages:
Stable friction coefficient
Suitable for Grade 10.9 applications
Reduced hydrogen embrittlement concerns compared with electrolytic coating processes
Better preload repeatability
Common applications:
Tracker bolts
Drive assembly connections
High-cycle structural joints
Hot-Dip Galvanized Fasteners
Hot-dip galvanizing according to ISO 1461 provides excellent corrosion protection for many structural applications.
However, friction characteristics are generally less controlled compared with engineered zinc-flake systems.
Potential issues:
Variable friction coefficient
Thread interference
Different torque requirements
Reduced preload consistency
For high-strength Grade 10.9 tracker bolts, coating selection requires careful engineering review.
Stainless Steel A4 Fasteners
A4-70 and A4-80 stainless steel fasteners provide excellent corrosion resistance but introduce different installation considerations.
Main concern:
Galling.
Thread galling can occur when stainless surfaces experience high friction during tightening.
Possible results:
Sudden torque increase
Thread seizure
Incorrect preload
For stainless solar clamps and coastal applications, installation speed, lubrication, and assembly procedure must be controlled.
4.4 Torque-Tension Testing Before Mass Installation
For critical solar structures, torque values should not be copied from standard tables without verification.
A proper torque-tension test evaluates the relationship between:
Applied torque
Achieved preload
The test confirms whether the specified installation torque actually produces the required clamp force.
Typical evaluation parameters:
Bolt diameter
Grade
Coating system
Lubrication condition
Nut type
Washer type
Standards such as ISO 16047 define torque/clamp force testing methods for fasteners.
4.5 Preload Requirements for Solar Tracker Fasteners
The target preload depends on:
Bolt diameter
Bolt grade
Joint design
Load condition
Example:
A Grade 10.9 M12 bolt may be tightened to achieve a preload in the range of approximately 50–70 kN depending on installation method and specification.
A larger M16 Grade 10.9 bolt may require preload levels above 90 kN.
The exact value must be determined by:
Structural calculation
Fastener specification
Manufacturer recommendation
4.6 Common Torque Control Methods Used in Solar Projects
Method 1: Torque Control
The most common field method.
Process:
Calculate required torque
Calibrate torque tools
Tighten according to procedure
Advantages:
Simple
Low equipment cost
Limitations:
Sensitive to friction variation
Method 2: Torque-Angle Control
This method combines:
Initial torque stage
Additional rotation angle
Advantages:
Better control in some applications
Less dependent on initial seating
Used where higher consistency is required.
Method 3: Direct Tension Control
This method measures bolt tension directly.
Examples:
Load indicating washers
Ultrasonic bolt measurement
Hydraulic tensioning systems
Advantages:
Direct preload measurement
Higher accuracy
Limitations:
Higher equipment requirements
4.7 Preload Loss During Solar Operation
Even correctly installed bolts can lose preload over time.
Common causes include:
Embedment Relaxation
Small surface irregularities flatten after installation.
Effect:
Initial preload reduction
Thermal Cycling
Solar structures experience daily temperature changes.
Expansion and contraction can affect joint behavior.
Vibration Loosening
Wind-induced movement can gradually reduce clamp force.
This is particularly relevant for:
Tracker systems
Rotating structures
High-wind areas
Corrosion
Corrosion products between connected surfaces can:
Change friction conditions
Reduce effective clamp force
Damage threads
4.8 Engineering Recommendations for Solar Fastener Preload Control
For EPC and solar mounting suppliers, a reliable preload management process should include:
Requirement Recommended Practice
Bolt specification Define grade according to ISO 898-1 / ISO 3506-1
Coating selection Specify ISO 10683 zinc-flake where required
Friction control Require torque-tension verification
Installation Use calibrated torque tools
Quality check Perform sample preload testing
Documentation Maintain batch traceability
4.9 Practical Example: Tracker Connection Failure Caused by Poor Torque Control
A tracker manufacturer may specify:
M12 Grade 10.9 bolt
Zinc-flake coating
Required preload
However, during installation, the contractor replaces the approved fastener with another coating supplier's product.
The bolt grade remains the same.
The appearance remains similar.
But the friction coefficient changes.
The same torque value now produces lower preload.
After several months of wind operation:
Joint movement increases
Bolt fatigue loading rises
Connection stiffness decreases
The failure was not caused by insufficient bolt strength.
The problem was loss of preload control.
4.10 Preload Is the Link Between Bolt Design and Structural Reliability
Solar mounting fasteners operate in a system where mechanical strength, corrosion protection, and installation control are connected.
A high-strength bolt without correct preload control cannot deliver its designed performance.
For utility-scale solar projects, especially single-axis trackers, engineers should specify:
Correct bolt grade
Suitable coating system
Verified friction characteristics
Controlled tightening procedure
Installation inspection requirements
The objective is not simply achieving a torque value.
The objective is creating a reliable bolted joint that maintains clamp force for decades of wind, vibration, and environmental exposure.
5. Wind Load and Fatigue Considerations for Solar Mounting Systems
[Image: wind-load-fatigue-analysis.jpg]
Solar mounting structures are designed for long service life, but the critical engineering challenge is not only the maximum wind load. The connection system must also survive repeated loading cycles caused by wind gusts, tracker movement, vibration, and thermal expansion.
For utility-scale PV projects, fasteners operate under a combination of:
Static structural loads
Dynamic wind pressure changes
Cyclic tension and compression
Connection slip forces
Environmental corrosion exposure
A bolt that passes a static strength calculation may still experience fatigue failure if the joint loses preload over time.
This is why solar fastener design must consider fatigue performance, preload retention, and vibration resistance together.
5.1 Wind Loading Effects on Solar Fastener Connections
Large photovoltaic arrays create significant aerodynamic loading.
Wind forces act on:
Module surfaces
Mounting rails
Torque tubes
Drive assemblies
Structural frames
The actual loading depends on:
Site wind speed
Terrain category
Array geometry
Tracker angle
Module orientation
Structural stiffness
Projects in MENA regions often face challenging conditions because many solar plants are installed in:
Open desert areas
High-wind zones
Coastal environments
Saudi Arabia, UAE, Qatar, and Oman solar developments commonly require fasteners capable of maintaining performance under strong wind exposure combined with dust and temperature cycling.
5.2 Static Strength Is Not Enough for Tracker Applications
Fixed-tilt PV structures mainly experience long-term static loading.
Single-axis trackers are different.
Tracker fasteners experience:
Daily rotation cycles
Wind-induced movement
Repeated actuator loads
Dynamic vibration
The critical factor becomes fatigue resistance.
Fatigue failure occurs when repeated stress cycles gradually create microscopic cracks that grow until fracture.
The key design parameters are:
Stress amplitude
Mean stress
Number of cycles
Surface condition
Thread geometry
Preload level
5.3 Fatigue Limit and Endurance Limit of Solar Fasteners
Two important engineering concepts are used when evaluating cyclic fastener performance.
Fatigue Limit
The fatigue limit is the stress amplitude below which a material can theoretically withstand a very large number of load cycles without fatigue failure.
Endurance Limit
The endurance limit describes long-duration cyclic loading capability under repeated stress conditions.
For solar tracker fasteners, maintaining bolt stress below the endurance limit depends on:
Correct bolt grade
Proper preload
Controlled friction
Suitable coating
Stable joint design
Why Grade 10.9 Is Preferred for Single-Axis Trackers
Grade 10.9 bolts are commonly selected for tracker applications because they provide:
Higher tensile strength
Higher yield strength
Higher achievable preload
Better resistance to joint separation
According to ISO 898-1:
Grade Tensile Strength Yield Strength Rp0.2
Grade 8.8 ≥800 MPa ≥640 MPa
Grade 10.9 ≥1000 MPa ≥900 MPa
The advantage of Grade 10.9 is not simply higher breaking strength.
The main benefit is that the connection can maintain a higher clamp force, reducing cyclic stress variation during operation.
Lower stress variation generally improves fatigue performance.
5.4 Vibration Resistance and DIN 65151 Junkers Test
Wind loading can create transverse movement within bolted joints.
When external forces overcome friction between connected components, the joint may experience:
Micro-slip
Preload loss
Self-loosening
The DIN 65151 Junkers transverse vibration test evaluates the behavior of bolted connections under controlled lateral vibration.
The test measures:
Initial clamp force
Preload reduction
Loosening behavior
Locking performance
For solar tracker applications, this type of evaluation is relevant because tracker structures experience:
Wind-induced vibration
Mechanical movement
Repeated dynamic loading
A reliable fastener system should maintain sufficient preload throughout operation.
5.5 Corrosion-Fatigue Interaction
Mechanical fatigue and corrosion are not independent problems.
In harsh environments, corrosion can accelerate fatigue failure.
Typical corrosion damage includes:
Thread pitting
Surface cracks
Reduced effective cross-section
Increased stress concentration
This is especially important in:
Coastal PV plants
Floating solar systems
High-humidity tropical regions
A corrosion-resistant coating protects not only appearance but also long-term mechanical performance.
5.6 Wind Load Fastener Design Checklist
Before approving a solar mounting fastener specification, engineers should confirm:
Item Requirement
Bolt grade ISO 898-1 Grade 8.8 / Grade 10.9 or ISO 3506-1 stainless
Fatigue requirement Evaluate cyclic loading conditions
Preload Defined installation target
Coating ISO 10683 zinc-flake or approved protection system
Friction Torque-tension data available
Vibration DIN 65151 evaluation where required
Documentation EN 10204 3.1 traceability
6. Common Installation Mistakes in Solar Fastener Projects
Correct engineering design can still fail if installation control is poor.
Many field issues found in solar structures are not caused by incorrect bolt selection. They result from:
Uncontrolled torque procedures
Wrong coating assumptions
Mixed fastener batches
Incorrect material combinations
6.1 Mistake 1: Selecting Grade 10.9 Without Considering Coating Risk
Grade 10.9 provides excellent mechanical performance, but it requires careful surface protection.
These bolts have:
Tensile strength ≥1000 MPa
High hardness
Quenched and tempered microstructure
High-strength steels are more sensitive to hydrogen embrittlement.
Hydrogen Embrittlement Warning: HDG and Grade 10.9 Fasteners
Hot-dip galvanizing according to ISO 1461 is widely used for structural steel protection.
However, using HDG on Grade 10.9 fasteners requires careful evaluation.
The risk comes from hydrogen entering high-strength steel during surface preparation processes before galvanizing.
Under high tensile stress, absorbed hydrogen may contribute to delayed cracking.
Possible failure characteristics:
Sudden fracture after installation
No obvious external warning
Failure occurring during service rather than assembly
For Grade 10.9 solar tracker bolts, many engineers prefer non-electrolytically applied zinc-flake coatings according to ISO 10683 because they are specifically designed for high-strength fasteners and avoid hydrogen generation associated with electroplating processes.
The coating selection should always follow project specifications and approved engineering requirements.
6.2 Mistake 2: Using Incorrect Torque Values After Changing Coating Systems
Torque values are not universal.
Changing from:
Zinc-flake coating
HDG
Plain steel
Lubricated stainless
changes friction behavior.
The same torque may produce completely different preload.
Engineers should verify:
Coating supplier
Friction coefficient
Torque-tension relationship
before installation.
6.3 Mistake 3: Ignoring Stainless Steel Galling
A4-70 and A4-80 stainless steel fasteners provide excellent corrosion resistance, but galling remains a common installation concern.
Causes include:
High tightening speed
Dry threads
Excessive torque
Incorrect lubrication
Results:
Thread seizure
Incorrect preload
Damaged components
6.4 Mistake 4: Mixing Fastener Batches
Large PV projects may require millions of fasteners.
Without batch control, problems can occur:
Different coating batches
Different friction coefficients
Different mechanical properties
A professional supply chain should maintain:
Heat number traceability
Production lot records
Inspection reports
6.5 Mistake 5: Treating Fasteners as Standard Hardware
Solar fasteners are structural components.
They require:
Material control
Mechanical testing
Coating verification
Installation procedures
The lowest purchase price does not always represent the lowest project cost.
7. How wffastener Supports Solar Hardware Projects
wffastener provides custom fastener manufacturing solutions for solar mounting systems, renewable energy structures, and power infrastructure projects.
The company supports EPC contractors, mounting system manufacturers, and project developers with engineering-focused fastener solutions.
7.1 Custom Fasteners According to Drawings
Solar structures frequently require customized components.
wffastener supports:
Special dimensions
Custom thread lengths
OEM fastener designs
Mounting hardware components
Drawing-based production
Engineering review covers:
Material selection
Manufacturing feasibility
Coating recommendation
Application requirements
7.2 High-Strength Solar Fastener Production
wffastener supports production of:
ISO 898-1 Grade 8.8 fasteners
ISO 898-1 Grade 10.9 fasteners
ISO 3506-1 A4-70/A4-80 stainless fasteners
Applications include:
Solar tracker systems
Ground-mounted PV structures
Module clamps
Structural joints
7.3 Surface Protection Solutions
Different environments require different coating strategies.
Solutions include:
Zinc-Flake Coatings
For:
Grade 10.9 tracker bolts
High-load applications
Controlled friction requirements
Standard reference:
ISO 10683
Zn-Al-Mg Coated Fasteners
For:
Desert solar structures
Cost-sensitive applications
Corrosion protection requirements
Stainless Steel Fasteners
For:
Coastal PV projects
Marine environments
Critical corrosion areas
7.4 Manufacturing and Quality Control
Fastener reliability depends on manufacturing consistency.
wffastener controls:
Raw material traceability
Thread accuracy
Heat treatment
Surface treatment
Dimensional inspection
For project approval, documentation support includes:
EN 10204 3.1 material certificates
Mechanical test reports
Inspection records
Coating documentation
8. Conclusion: Solar Reliability Starts With the Fastener System
A solar mounting structure depends on thousands of individual connections working together for decades.
The correct fastener solution requires balancing:
Mechanical strength
Preload capability
Fatigue performance
Corrosion resistance
Installation control
Grade 8.8 remains suitable for many fixed PV applications.
Grade 10.9 provides advantages for single-axis trackers and high-cycle connections when combined with appropriate coating systems such as ISO 10683 zinc-flake protection.
A4-70 and A4-80 stainless fasteners provide reliable performance where chloride exposure and marine corrosion risks dominate.
The engineering goal is not selecting the strongest or most expensive bolt.
The goal is selecting the correct fastener system for the actual operating environment.
9. Frequently Asked Questions
Q1: Why are Grade 10.9 bolts used in solar tracker systems?
Grade 10.9 bolts provide higher tensile strength and yield strength compared with Grade 8.8 bolts. This allows higher preload levels, improving joint stiffness and fatigue performance under repeated wind loading.
Q2: Why is zinc-flake coating preferred for Grade 10.9 solar bolts?
Grade 10.9 fasteners exceed 1000 MPa tensile strength and require careful corrosion protection. ISO 10683 zinc-flake coatings provide corrosion resistance with controlled friction characteristics and are commonly selected for high-strength fasteners.
Q3: Can Grade 10.9 bolts be hot-dip galvanized?
HDG should be carefully evaluated for Grade 10.9 fasteners because high-strength quenched and tempered steels are more sensitive to hydrogen-related failure risks. Project specifications should define acceptable coating systems and inspection requirements.
Q4: What is the difference between A4-70 and A4-80 stainless fasteners?
Both are corrosion-resistant stainless fasteners according to ISO 3506-1.
A4-80 provides higher mechanical strength:
A4-70: tensile strength ≥700 MPa
A4-80: tensile strength ≥800 MPa
A4-80 is often selected where higher loads and corrosion resistance are required.
Q5: How should EPC contractors evaluate a solar fastener supplier?
A professional evaluation should include:
Material certificates
Mechanical test reports
Coating specifications
Torque-tension data
Batch traceability
Production capability
Sample approval process
10. Tiered CTAs
Tier 1: Download Solar Fastener Engineering Selection Matrix
Receive a technical reference covering:
Grade 8.8 vs Grade 10.9 selection
A4 stainless applications
Coating recommendations
Preload requirements
Tracker fastener specifications
Tier 2: Request Solar Fastener Sample Evaluation Package
Receive project samples with:
Material certificates
Mechanical test reports
Coating documentation
Dimensional inspection records
Recommended installation parameters
Tier 3: Submit Solar Tracker Drawings for Custom Fastener Quotation
Send your:
Mounting structure drawings
Fastener specifications
Project environment details
Quantity requirements
WhatsApp Engineering Support: +86 XXX XXXX XXXX (for MENA urgent technical inquiries)
wffastener engineers can support:
Fastener selection
Manufacturing feasibility review
Surface treatment recommendation
Production planning
Technical documentation preparation
Reliable solar structures begin with correctly engineered fastener connections.